Injection Moulding Defects: Causes, Fixes and Which Ones Start in the Mould
On this page
Every moulder sees defects: a part that does not fill, a thin line of flash at the lid, a dent behind a rib. The useful question is not only “what is this defect?” but “where does it start?” Some defects are fixed in minutes by changing machine settings. Others come from the mould itself (the gate, the venting, the cooling or the part design) and no setting will remove them for good.
This guide covers the injection moulding defects buyers ask us about most often: what each one looks like, what usually causes it, how to fix it at the machine, and when the fix has to be made in the mould.
Machine settings or mould: how to tell where a defect starts
Before changing anything, look at the pattern. A few simple checks point you in the right direction:
- Same place, every shot, whatever the settings: the cause is usually in the mould or the part design (gate position, a missing vent, a thick section, a hot spot in the cooling).
- Comes and goes with temperature, speed or a new material lot: the cause is usually the process or the material.
- Only one cavity of a multi-cavity mould: look at that cavity’s venting, cooling and runner balance. The machine treats all cavities the same, so a single bad cavity points at the mould.
- Appeared after months of good production: check for wear (parting line, shut-offs, vents filled with residue) and blocked cooling channels.
Change one setting at a time and note the result. Changing three things together hides the real cause.
Common defects at a glance
| Defect | What you see | Usual process causes | Usual mould or design causes |
|---|---|---|---|
| Short shot | Part not completely filled | Too little material, low pressure or speed, cold melt | Gate too small or too far, poor venting, unbalanced runner |
| Flash | Thin film of plastic at the parting line or around pins | Too much pressure, melt too hot, clamp force too low | Worn or badly fitted parting line, damaged shut-offs, weak plate support |
| Sink marks | Shallow dents on the surface | Low hold pressure or short hold time | Thick ribs or bosses, gate far from thick areas, poor cooling |
| Warpage | Part bends or twists after ejection | Uneven mould temperature, ejecting too hot | Uneven wall thickness, unbalanced cooling, gate position |
| Weld lines | Thin line where two flow fronts meet | Low melt or mould temperature, low speed | Gate position, holes or cores in the flow path, no vent at the weld |
| Flow marks and jetting | Wavy lines or snake-like marks near the gate | Wrong injection speed, cold melt | Small gate pointing into open space |
| Burn marks | Brown or black marks at the end of fill | Injection too fast at the end of fill | Trapped air, missing or blocked vents |
| Silver streaks | Silvery streaks in the flow direction | Wet material, overheated material | Rarely the mould |
| Ejector marks and stress whitening | Shiny or white marks where pins push | Ejecting too early or too fast | Too little draft, rough polish, too few ejector pins |
Short shots
A short shot is a part that is not completely filled, often at the far corners, thin ribs or the last cavity of a multi-cavity mould. At the machine, check that the shot size is enough, then raise injection speed or pressure and check the melt and mould temperatures against the material supplier’s data. A partly blocked nozzle or a feed problem in the hopper gives the same symptom.
If the same spot stays short at every setting, look at the mould: trapped air that cannot escape (add or clean the vents), a gate that is too small or freezes too early, very thin walls far from the gate, or a runner that fills one cavity before the others. Thin-wall parts such as plastic food container moulds are especially sensitive, which is why gate size, venting and runner balance are planned in the mould design rather than left to the machine operator.
Flash
Flash is a thin film of plastic that escapes where the mould halves meet, around ejector pins or along slides. On the machine, reduce injection or hold pressure, lower the melt temperature and check that the machine’s clamp force is enough for the projected area of the part. A mould running on a machine that is too small will flash however well it is made.
When the flash appears in the same place on a well-set machine, the mould needs attention: a worn or damaged parting line, a shut-off that no longer seals, plates that bend under pressure because they lack support pillars, or vents cut too deep. These are workshop fixes, not setting changes.
Sink marks and voids
Sink marks are shallow dents, usually opposite a rib, boss or thick corner. Plastic shrinks as it cools, and a thick section keeps shrinking after the skin has set, pulling the surface in. If the skin is strong enough, the shrinkage shows up inside instead, as a void (an air-like bubble in a clear or cut part).
Longer hold time and higher hold pressure help, as long as the gate stays open long enough to pack the part. The lasting fix is in the design and the mould: ribs thinner than the wall they support, cored-out bosses, gates placed near the thick sections, and cooling channels close to the hot spots.
Warpage
A warped part comes out of the mould straight and then bends or twists as it cools. The cause is uneven shrinkage: one side cools faster than the other, or thick and thin areas shrink by different amounts. Longer cooling and equal mould temperatures on both halves reduce it.
Large flat parts such as crates, trays and tool box lids warp most easily. For these, the cooling layout, the gate positions and an even wall thickness matter more than any setting. When we plan plastic crate moulds, the cooling is laid out around the base and corners so the crate stays flat and stacks properly.
Weld lines and flow marks
When plastic flows around a hole or a core, the two flow fronts meet again on the other side and leave a weld line. It can be a cosmetic problem and also a weak spot. Higher melt and mould temperatures and a faster fill make the fronts join better. In the mould, the gate can be moved so the weld line forms where it does not matter, and a vent at the weld lets trapped air escape.
Flow marks are wavy lines near the gate, usually from a melt or mould that is too cold or the wrong injection speed. Jetting is a worm-like mark that appears when plastic shoots from a small gate straight into open space. The fix for jetting is mostly in the mould: gate into a wall or use a wider gate so the plastic spreads instead of squirting.
Burn marks and gas marks
Brown or black marks at the end of fill, often in corners or at the last point to fill, come from air that is trapped and compressed so fast that it heats up and scorches the plastic. Slowing the injection speed near the end of fill helps for a while. The real fix is venting: clean vents that are blocked with residue, or add vents where the air has nowhere to go. Because these marks appear in the same place every shot, they are one of the clearest signs that the mould needs work.
Silver streaks, discolouration and black specks
Silver streaks (also called splay) run in the flow direction and usually mean the material was not dried properly. Materials such as ABS, PC and nylon absorb moisture from the air and need drying as per the supplier’s datasheet. Discolouration and black specks come from overheated material, plastic sitting too long in a barrel that is too big for the shot, or contamination from a dirty hopper or a colour change. Lower the temperature, purge the barrel and keep the material handling clean. These defects are almost never caused by the mould.
Ejector marks and stress whitening
If the part sticks to the core, the ejector pins have to push hard and leave shiny marks or white stress marks. Check that the part is cool enough before ejection and that the ejection speed is not too high. In the mould, the causes are too little draft, a polish that is rough or runs across the direction of ejection, or too few ejector pins for the area. Deep, thin-wall parts such as containers and cups often eject better with a stripper plate or air valves than with pins alone.
How a mould trial catches defects before dispatch
The cheapest time to fix a mould defect is before the mould leaves the workshop. We run every new mould on an injection moulding machine and send the buyer videos and photos of the trial and the moulded parts before dispatch. If the trial shows a defect that comes from the mould, such as a flash line at the parting line or a burn mark from missing venting, it is corrected in our workshop first. You can read how each mould moves from design to trial on our process page.
When you look at trial videos and photos of a new mould, check these points:
- Every cavity fills completely, including thin ribs and corners.
- No flash at the parting line, around lids or along slides.
- No sink marks behind ribs, handles or bosses on the faces that matter to you.
- Parts come off the core without sticking or deep ejector marks.
- Lids fit their containers, and flat parts lie flat.
For larger industrial parts, our guide to common challenges in industrial mould manufacturing goes into fit, wall thickness and cooling in more detail.
Frequently asked questions
What are the most common injection moulding defects?
Short shots, flash, sink marks, warpage, weld lines, flow marks, burn marks, silver streaks and ejector marks. Most moulders see all of them at some point; the skill is in finding whether the cause is the setting, the material or the mould.
Can a defect be fixed without changing the mould?
Often, yes. Defects that change with temperature, speed, pressure or material lot can usually be fixed at the machine or in material handling. A defect that stays in the same place on every shot, whatever the settings, normally needs work on the mould or a change in the part design.
Which defects should the mould maker fix?
Burn marks and short shots from poor venting, flash from a parting line or shut-off that does not seal, short shots from an unbalanced runner, and sink or warpage caused by cooling that does not reach the thick areas. Design-related causes, such as a rib that is too thick, are best agreed before steel is cut.
How do you check for defects in a multi-cavity mould?
Number the cavities and keep the parts from each cavity apart. If one cavity is always short or always flashes, the cause is in that cavity’s gate, venting or runner. Our guide to single cavity vs multi-cavity moulds explains why runner balance matters when you add cavities.
Planning a new mould?
Many defects are avoided at the design stage, before any steel is cut. Send us your drawing, sample or photos with the plastic and the quantity you plan to make through our enquiry form. Every mould is made to order, the 3D design is shared with you for approval, and you see the mould working in trial videos and photos before dispatch.
For a deeper technical reference, see the moulding defects table on Wikipedia’s injection moulding article and RJG’s guide on troubleshooting common defects in injection moulded parts.
Planning a mould?
Send your drawing, sample or photos. Every mould is made to order and trialled before dispatch.
We design and make plastic injection moulds in Kathwada GIDC, Ahmedabad: 8+ years in business, steel moulds (P20, H13, EN31, S136), every mould trialled before dispatch. About us · Our process
Related guides
Plastic Injection Mould: A Complete Guide for Buyers
What a plastic injection mould is, how it works, the main types and parts, mould steel, design, the trial, cost and delivery time, with links to…
Food-Grade Plastic Moulds in India: Material and Safety Basics
Short answer: "food-grade" mostly describes the plastic and the finished container, not the steel mould. A good food-grade mould is one that is built, finished and…
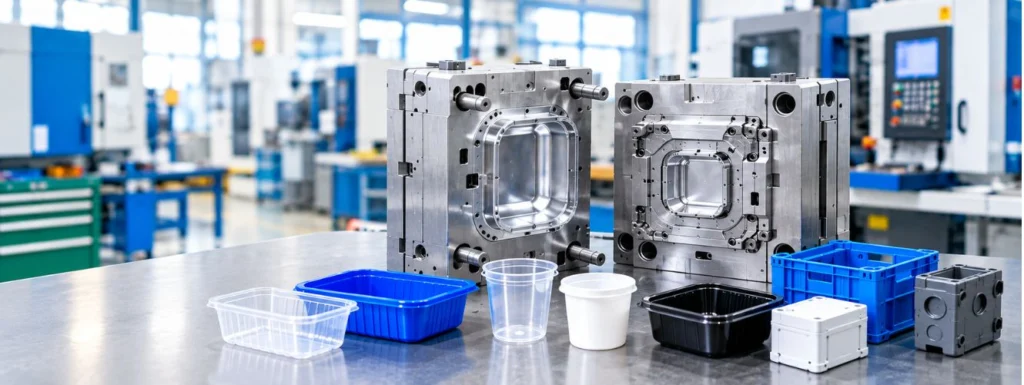
How to Choose the Right Plastic Injection Mould Manufacturer for Your Product
IntroductionPicking a Plastic Injection Mould Manufacturer is one of the biggest decisions for any business that uses Plastic Injection Moulding. The quality of the mould directly…